Every mechanical motion needs a power source, and the drive on a printing press has to do more than turn a shaft. It must hold a steady speed, answer the operator, and offer continuous speed adjustment as the job changes. Before shaftless drives arrived, newspaper presses passed through two generations of electric speed control. Slip-ring AC motors dominated until the 1970s and can be called the first generation. From the 1970s, progress in DC speed control brought DC drives and slip motors into wide use, the second generation. The picture changed in 1992, when Rexroth built SYNAX, the first shaftless drive system designed for a printing press. Within a decade, shaftless speed control had replaced the older methods on newspaper presses.
Shaftless drives as a new press concept
Shaftless transmission has become a fresh concept in press engineering. It breaks the limits that a common mechanical shaft places on machine layout, and it opens room for new designs in both press development and press manufacturing. The technology dates from that 1992 SYNAX system and has since spread to a number of drive specialists worldwide.
Communication standards inside a shaftless drive
The system is built on distributed intelligence and follows SERCOS, the Serial Real time Communication System, an international drive communication standard. Control information travels digitally in real time over optical fibre. Each group of motors uses a distributed intelligent card that can manage 40 motor positions, and the cards can be linked by fibre to form a control group covering as many as 1000 positions from 32 connected cards.
How the units stay in sync
Synchronization rests on three parts: an intelligent digital frequency converter, AC motors, and a 32-bit digital encoder with closed-loop feedback. The encoder system corrects motor position 4000 times per second, while the frequency converter steps the AC motor in units numbering two million. Fibre optic digital transmission over an Ethernet interface carries that data with the resolution and register accuracy that printing quality demands.
What shaftless drive brings to press control
Distributed and modular drive design. Multi-web configurations can use smaller drive units. On a Roland single-circumference, double-diameter eight-colour tower press, for example, the drive motors moved from a single motor of 90 kW or more to individual motors of 27 kW or less, and the shock on the electrical grid at start-up fell by more than three times.
Register error from mechanical transmission disappears. Published figures for a press with eight printing units show that the variation between unit 1 and unit 8 can be seven times greater than the variation between unit 1 and unit 2, because every mechanically synchronized part carries its own tolerance. That error only fades once gears and shafts reach continuous rotation.
Makeready time drops. Each colour unit can be driven on its own, so several people can prepare the press at the same time. A Roland eight-colour tower press uses four drive motors, and a KBA eight-colour tower press uses eight.
Control becomes interchangeable. Because the system uses an international drive communication standard, no shaftless press carries a patent restriction on information transfer.
Fault diagnosis is dependable. With SERCOS, the manufacturer can store the standard operating parameters in the system, collect live parameters from the press, and compare the two to locate a fault.
Speed regulation on the drive rollers reaches an accuracy of 0.01 percent, which allows precise control of pull roller speed, stable web travel, even tension, and consistent cutting across multiple webs.
Positioning accuracy raises the reliability of automatic plate changing and shortens the reaction time of printing and cutting register, which cuts waste.
Variable-frequency speed control and the three-phase motor
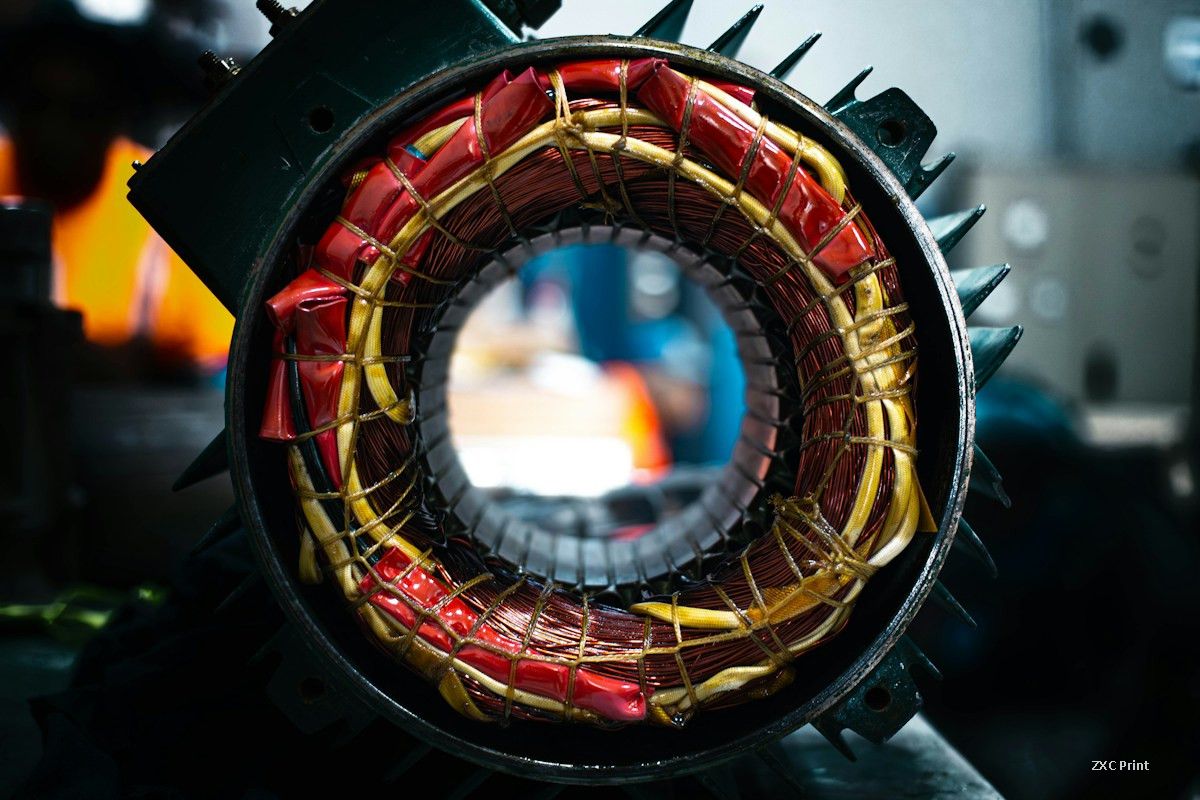
Shaftless press drive depends closely on variable-frequency speed control. That technique works with the main characteristics of a three-phase asynchronous motor, whose speed follows n = 60f/p. Speed n is set by the current frequency f and the number of magnetic pole pairs p, and the pole pairs cannot be altered once the motor is built. Motor speed is therefore proportional to frequency, and a variable-frequency drive uses exactly that relationship to set the output speed.
The AC variable-frequency drive on a press
In the late 1980s a new field effect transistor, the IGBT, improved the behavior of variable-frequency motors, and presses began to adopt variable-frequency drive control. The arrangement combines an inverter with a three-phase asynchronous motor and most often uses the AC-DC-AC voltage type. That type suits constant current control, which matches the constant torque demand of a press, and it runs at low power, so industrial control also calls it AC servo control. The cycle has two stages. First, the fixed-frequency three-phase supply is rectified into DC. Second, the DC is inverted back into AC, and controlling the frequency of that inverted output controls motor speed. The inverter bridge on a shaftless drive uses IGBT circuits, which are voltage-controlled devices with low control power and switching frequencies up to 20 kHz. The result is a current waveform closer to the mains supply, a motor that keeps more of its three-phase behavior, less electromagnetic noise, a simpler circuit, better self-handling of common faults, a lower failure rate, and lower losses in the inverter itself.
Three ways to control AC variable-frequency drive
Press structure makes the load uneven, yet printability requires smooth running for consistent quality. Two practical questions follow: does the change from DC to AC drive alter the printed result, and how are motors synchronized when some carry encoders and others do not?
Vector control. A DC motor turns on two perpendicular magnetic fields, and controlling one field controls both speed and mechanical behavior. A three-phase asynchronous motor only holds a perpendicular field for an instant. Vector control addresses the inverter bridge so that the instantaneous perpendicular field is controlled. The first step splits the setpoint signal into two rotating DC components, the magnetic field component iM and the torque component iT. The second step transforms those components, using the motor parameters, into the control signals iA, iB and iC for the three-phase inverter bridge.
Vector control without feedback. A common motor type on shaftless presses carries no encoder, but it does not run as open-loop control without speed regulation. Synchronization comes from measuring terminal voltage and current, calculating rotor flux and rotor angular speed, and using those values with the motor parameters in the same transformation. Dynamic response is slightly weaker, and a press that uses this control on its colour register motors may show small register differences as speed changes.
Vector control with feedback. Where printability demands exact speed control, such as setting the production speed or holding colour register speed, an encoder is fitted directly on the motor. It reports rotor speed for the transformation and keeps motor speed tightly matched to the setpoint. Dynamic response is strong, and register does not shift as speed changes.