
How to Reduce Color Difference in Finished Printed Products
Color difference complaints are among the most persistent headaches in printing and packaging, and the pressure is highest for plants that live on export orders. Anyone who has worked with color management will say the same thing: standardization and stability sit underneath every method and every standard in the field. Post-press operations are a large part of that picture, and the notes below explain how they shift color and what a plant can do about it.
How Post-Press Operations Move the Color
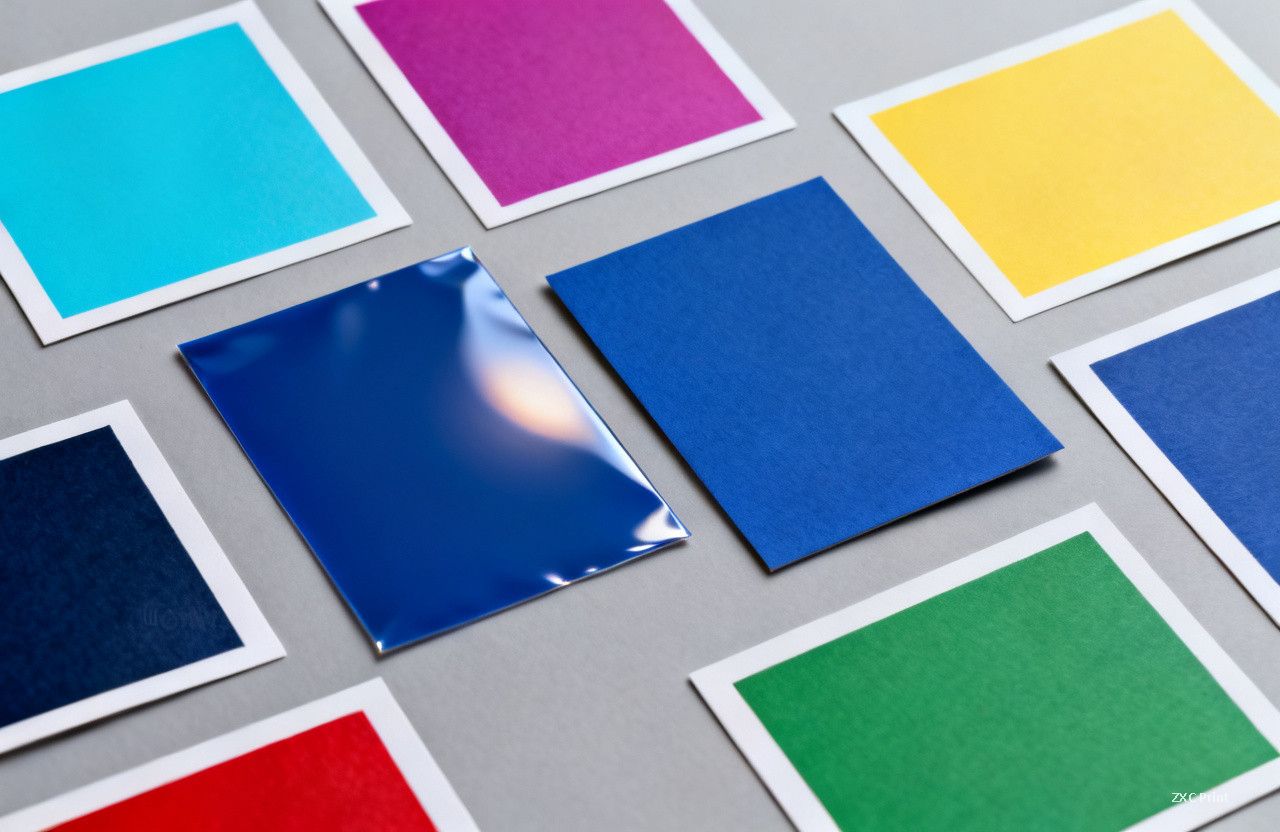
A sheet that leaves the press is not the sheet the customer receives. Lamination, varnish, UV coating, aqueous coating and embossing all change the way light behaves at the surface of the print. Gloss lamination deepens the darker tones and adds contrast. Matte lamination flattens them and lifts the midtones. Aqueous coating alters surface energy and slightly darkens the sheet. The ink film itself does not change, but the measured value and the perceived color both do. That is why a proof approved without finishing can look wrong once the finished product is placed next to the customer's approved sample.
Standardize Materials Before Chasing Numbers
The first lever is not software. It is the material list. Keep the brand and the type of every surface treatment consumable the same from job to job, and check incoming stock against its specification instead of trusting the label. Film thickness and film color matter more than most plants expect. A batch of lamination film that runs a few microns thin, or slightly warmer in tone, will move the final color even when the press is perfectly under control. Holding brand and model constant is already difficult in real production, and adding incoming inspection makes it harder. Weighed against the cost of a color complaint, a reprint and a delayed shipment, the effort is cheap.
Build Two ICC Profiles, Not One
Once material control is in place, the second step is to separate the two states of the product inside color management. A plant should hold two ICC profiles: one describing the process with surface finishing, and one describing the process without it. They are used at different points in the workflow.
- During prepress color matching, compare the customer's color sample against a digital proof built with the finishing profile, because that proof predicts the appearance of the finished goods.
- After the match is accepted, output two digital proofs from the same data.
- On press, follow the proof made without surface finishing. Hold the press sheet to that target, and the finishing step will bring the printed sheet back into line with the customer's sample.
What Color Management Cannot Fix
Color management is a powerful tool with hard limits, and those limits are worth stating plainly.
- A managed workflow cannot widen a device gamut. It maps one color space into another, so an arbitrary customer file cannot always be reproduced exactly as supplied. Some colors sit outside what the press can lay down.
- Gamut mapping always loses something. When a target color falls outside the achievable range, the plant must decide whether accurate hue or minimal visual shift matters more, and that decision belongs with the customer.
- Digital proofing targets one press or one printing standard. A proof built for a coated sheet on a five-color machine does not transfer to a different press, a different substrate or a different ink set. Treating every machine as if it can follow the same proof is a common source of disputes.
- Metamerism deserves attention in every color routine. Two samples can match under one light source and diverge under another, so approving a color under a single lamp will not reveal the problem.
The Operator Still Decides the Outcome
Tools and profiles set the target, but people hit it. An experienced prepress operator, pressman and finishing hand can deliver work that a weaker team cannot, even with identical equipment and identical standards. Competent staff working inside a defined color management system outperform a sophisticated system run without judgment. The practical aim of color management is to make good results repeatable for operators who are still learning, so a growing team can reproduce color consistently and spend less time and less material on the way to an acceptable sheet. The same system lets color move between input and output devices, and it shortens the conversation between prepress, press and finishing.
Standards Apply to the Equipment Too
An old saying holds that a craftsman must sharpen his tools before he can do good work. In color management, standardization and stability are asked of the operator, but they are asked of the software, the measuring instruments, the profiles and the workflow as well. If a spectrophotometer drifts, if a monitor is calibrated monthly instead of weekly, or if a profile is quietly replaced, discipline on the factory floor cannot compensate. Color management and quality management reinforce each other. When both are working, the plant can predict color instead of discovering it, quality holds steady across shifts, and customer complaints fall away. Believe the system, but do not treat it as a guarantee. A managed workflow removes many of the problems, not all of them, and the judgment of a good operator remains part of the answer.